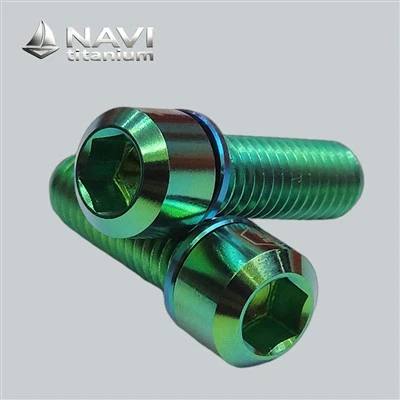
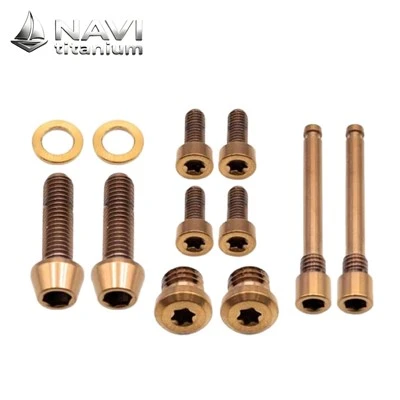
NAVI Titanium M5 titanium stem bolts are CNC-machined fasteners that pull the handlebar into the stem clamp on motorcycles and bicycles, locking bar, stem and steerer into one rigid assembly. For distributors, workshops and OEM assembly lines, NAVI Titanium treats that small part as a sellable upgrade, not hardware filler: stocked M5 sizes ready to ship, mixed head styles inside one order, own-brand packing, and a quotation returned against your drawing inside one working day. Grams saved at the cockpit are grams the rider feels in steering response, which is why this line sells at margins steel hardware never reaches.


Solutions of NAVI Titanium
M5 bolts earn their place where a plain steel clamp screw only adds mass at the one spot a rider notices. The stem sits ahead of the hands, so grams there show up in steering feel, while road salt, sweat and wet winter storage leave steel hardware stained and seized inside the clamp. Titanium carries roughly half the density of steel yet still holds clamp load through repeated torque cycles, and it does not galvanically attack a carbon bar or carbon steerer the way aluminium and steel fasteners can. Grade, pitch and bearing face must match the stem maker's callout. The NAVI Titanium Materials & Titanium Alloys table below sets out the titanium grades we machine here most often.


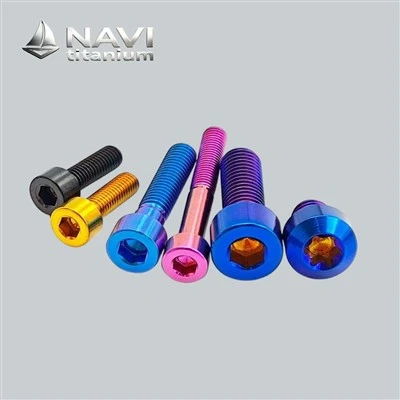
M5 bolts leave our shop in socket-cap, button, countersunk, flanged and tapered head profiles, with hex-socket, Torx or hexalobular drives and matching titanium washers. Shank length, thread pitch, shoulder step and under-head radius are cut to your drawing, so hidden-fixer caps, custom collars and non-standard clamp covers can be reproduced from a sample piece or a STEP file.


Application
Two faults decide whether a stem clamp screw gets pulled: threads that gall and lock during torque-up, and preload that bleeds away under engine buzz or trail chatter until the bar creeps. A third is galvanic: steel or aluminium hardware against a carbon bar pits and can creep-damage the clamp bore, a couple titanium removes. Each is avoided only when grade, pitch, bearing face and torque method match the stem. The two duties below are the installations we machine most.
Motorcycle Handlebar Clamps, Risers & Lever Perches
On motorcycles, M5 and M8 clamp hardware holds the bar into the riser, the riser into the triple clamp, and the brake and clutch lever perches onto the bar itself. A single-cylinder engine feeds continuous buzz into exactly those joints, and a bolt that loses preload there lets the bar rotate under hard braking, a pothole or a kerb strike.
Steel clamp bolts also seize in the riser after two winters of road salt, so a routine bar swap turns into a drilling job and a ruined riser. M5 titanium stem bolts keep the clamp serviceable, shed roughly forty per cent of the fastener mass at the highest, most remote point of the machine, and stay free in the thread where steel would rust solid.
Torque must be set with a calibrated wrench, threads prepared with anti-seize paste, and the maker's figure treated as a ceiling rather than a target.


Bicycle Stem Faceplates, Carbon Bars & Cockpit Hardware
On bicycles the four-bolt stem faceplate is the most fatigue-loaded fastener group a rider touches, and on a carbon bar it is also by far the most sensitive one.
Steel and aluminium bolts in contact with carbon fibre set up a galvanic couple that pits the metal and can creep-damage the bar around the clamp bore; titanium sits close enough to carbon on the galvanic scale to be the safe choice, which is why premium stems specify it.
M5 × 0.8 pitch in 16–20 mm lengths covers the majority of road, gravel, XC and e-bike stems, and a full cockpit swap of faceplate, steerer clamp and bar-plug hardware typically removes 25–40 g right where the rider feels it most.
Faceplate bolts must be tightened in a cross pattern, in stages, to the bar and stem maker's stated limit, with a gap check on both sides of the clamp.
Purchasing guide

Quality control (QC)
NAVI Titanium machines M5 bolts under an ISO 9001 system, with titanium bar stock released against its mill certificate before the first cut. Orders are checked for grade, thread pitch, length, head profile, tolerance and finish, and out-of-callout parts are scrapped, not sorted. Material and inspection records travel with the goods. Click the button to view the COA.

Titanium Bolts Manufacturing Process
NAVI Titanium M5 titanium stem bolts are manufactured through a complete standardized precision production process, with strict quality control implemented from raw material incoming inspection to finished product packaging. Every working procedure adopts professional titanium processing technology, avoiding ferrous contamination, ensuring stable mechanical properties, precise dimensional tolerance, excellent fatigue resistance and consistent appearance of each bolt. Strict batch inspection and record management guarantee high-quality, high-reliability customized titanium fasteners for motorcycle modification and industrial supporting scenarios.
|
Process Step |
Detailed Manufacturing & Quality Control Standard |
|---|---|
|
1. Bar Stock Release & Identity Check |
Titanium bar arrives with a mill heat number and certificate. Each length is checked for diameter, straightness and surface condition, and the alloy identity is confirmed before it enters the machining cell. Titanium and steel tooling are kept in separate, clearly marked areas so no ferrous contamination reaches a finished bolt. |
|
2. Cut To Length & Head Forming |
Bar is cut to blank length on a saw with coolant matched to titanium, then the head is formed. Standard profiles are cold-headed to keep grain flow running through the head-to-shank radius; low-volume or non-standard heads are turned complete from solid bar. |
|
3. CNC Precision Turning |
Shank diameter, shoulder step, under-head radius and any washer face are turned to drawing. The under-head radius is the detail that decides whether a bolt seats square or cocks in a countersunk clamp bore, so it is cut to tolerance rather than left to the tool nose. |
|
4. Thread Rolling (Not Cutting) |
Threads are rolled, not cut. Rolling displaces material into the root and flank, work-hardens the surface and keeps grain flow continuous, which gives a stem bolt cleaner threads and better fatigue behaviour than a cut thread at the same pitch. Go/no-go gauging follows on every batch. |
|
5. Heat Treatment & Surface Finishing |
Grade 5 blanks receive solution treatment and ageing, or stress relieving where the drawing calls for it, with furnace records kept against the lot. Surfaces then finish plain, polished, anodised to colour or PVD-coated, depending on the order. Colour anodising is matched across a set so a four-bolt faceplate looks uniform. |
|
6. Final Inspection & Packaging |
Every batch is read for thread fit, length, head dimensions, surface and drive recess. Sample pieces are pulled for tensile and hardness checks, and torque-to-seize trials run where the customer specifies them. Bolts are bagged by set, wrapped so heads cannot touch, and boxed with the lot number on the label. |
Titanium Fasteners (M5/M8 Stem Bolts)
The figures below are drawn from published material data and in-house production records for reference only; values shift with lot, heat treatment and supplier, and every shipped order is confirmed against its own certificate rather than this table. Use it only for shortlisting a material, then let the drawing and the COA settle the final call for your own order.
| Comparison Item | Ti-6Al-4V (Gr5) | Titanium Gr2 | Stainless A2-70 | Alloy Steel 12.9 | Aluminium 7075-T6 |
|---|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 4.51 | 7.90 | 7.85 | 2.81 |
| Tensile strength (MPa) | 950–1100 | 345–450 | 700 | 1200 | 540–570 |
| Yield strength (MPa) | 880 | 275 | 450 | 1080 | 470–505 |
| Elastic modulus (GPa) | 110 | 105 | 193 | 210 | 72 |
| Mass of four M5×18 bolts (g) | ≈ 6.0 | ≈ 6.1 | ≈ 10.8 | ≈ 10.7 | ≈ 3.8 |
| Behaviour in salt spray | No rust | No rust | Pitting risk | Rusts unprotected | Pitting risk |
| Galvanic behaviour against carbon fibre | Compatible | Compatible | Attacks carbon | Attacks carbon | Severe attack |
| Thread galling tendency | High without lube | High without lube | Moderate | Low | High |
| Torque retention under vibration | Good with lube | Fair | Fair | Good | Poor |
| Colour anodising possible | Yes | Yes | No | No | Yes |
| Relative material cost index | 6–8 | 5–7 | 1.5 | 1 | 2 |
| Verdict for stem duty | Best all-round | Light duty only | Heavy, pits | Heavy, rusts | Not for clamp duty |
Everything Under One Roof, From Bar Stock To Boxed Freight
In-House Equipment, No Subcontracted Machining
Sintering furnaces, CNC turning centres, thread rolling and a tool and die shop sit inside the NAVI Titanium plant, so M5 bolts never leave our control for outside processing. That matters on a clamp bolt, because head seating, thread root quality and heat treatment decide whether the fastener holds preload, and each is easier to control when one team runs every step. Buyers get a single accountable contact, one schedule and one inspection record. Lead times hold because no slot depends on a subcontractor's queue, and quality holds because nothing is accepted from a workshop we cannot audit.
Sample Service: Try Before You Commit
Free sample pieces and small trial runs are available on M5 titanium stem bolts, so a workshop or distributor can torque, vibrate and salt-test the hardware on their own stems before releasing a bulk order. Send a drawing, an original bolt or a marked photograph with thread size and length,


and we machine to that reference first. Once the sample clears your own fitting and torque checks, the approved specification is filed against your account and repeat lots are cut to it. The route suits aftermarket brands building a hardware line and OEM buyers qualifying a second source at volume.
Capacity, Delivery & Export Packing
Steady batch capacity covers both catalogue M5 stock and drawing-led runs, with schedules agreed at order confirmation rather than left open. Finished bolts are packed by set, separated so heads and threads cannot scuff each other in transit, and cartons carry lot numbers that tie back to inspection records.
Shipments move by sea or air to Europe, North America, Japan, Southeast Asia and the Middle East, with export documents prepared alongside the goods. Mixed M5, M6 and M8 consignments are routine for distributors stocking a full clamp range, and repeat orders are scheduled against the specification already held on file.
FAQ
1. Will an M5 bolt fit my motorcycle or bicycle stem?
-
Match three numbers: thread pitch, shank length under the head, and head profile. Most bicycle stem faceplates take M5 × 0.8 in 16–20 mm lengths, while motorcycle risers and lever perches run M6 or M8. Send the original bolt or a photograph with measurements and we confirm fitment first.
2. Do I torque titanium the same as the steel bolt I removed?
-
No. Titanium galling under dry, fast torque-up is the usual complaint, so threads need anti-seize and a slow pull with a calibrated wrench. Treat the stem maker's figure as a ceiling, and follow the bar's limit on carbon. German and Japanese buyers often ask for the DIN or JIS basis.
3. How long do these bolts last, and what maintenance do they need?
-
Titanium does not rust, so in coastal and winter-salted markets service life is usually set by the bar or the stem, not the bolt. Re-check torque after the first ride, then at each service interval. Retire any bolt showing thread damage, distortion or a head that no longer seats square.
4. How do I remove a seized original steel bolt and fit the titanium set?
-
Penetrating oil, gentle heat cycles and patience come first; drilling is the last resort. Clean the clamp thread out, chase it if needed, then fit the titanium bolts with a little anti-seize, tighten in a cross pattern in stages, and confirm an even clamp gap on both sides before riding.
5. What paperwork proves the material and the quality of my order?
-
Each lot ships with a certificate of analysis covering alloy, mechanical data, dimensions and quantity. European buyers usually ask for EN 10204 3.1 papers, North American buyers for ASTM or AMS references, both available on request. Use the COA button on this page to view the current document set.
Hot Tags: m5 titanium stem bolts, China m5 titanium stem bolts manufacturers, suppliers, factory