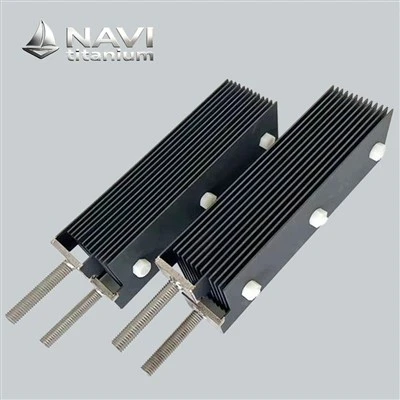


NAVI Titanium self-developed MMO coated titanium anode for electrolysis cell is a dimensionally stable anode (DSA) made from high-purity titanium substrate with a thermally decomposed mixed metal oxide catalytic layer. We fully control the entire production process, including substrate cutting, forming and welding, pretreatment, precious metal coating sintering, and performance testing. We support customization in plate, mesh, and pipe structures, coating formula adjustments, and processing according to electrolysis cell drawings. We offer bulk procurement, trial orders, and OEM support to electrolysis equipment manufacturers, water treatment system integrators, chemical equipment companies, and engineering contractors.
Solution of NAVI Titanium
NAVI Titanium leverages its mature coating development and precision manufacturing technology to create a series of MMO titanium anode products tailored to different electrolyte environments, current densities, and usage needs, ensuring an exact match between coating solutions and application scenarios, and overcoming the common issues of generic anodes like poor adaptability, rapid decay, and short lifespan.


Application
MMO coated titanium anode for electrolysis cell, produced by NAVI Titanium, allows current to pass into the electrolyte, where chlorine, oxygen, or other oxidation reactions occur on its surface, converting electrical energy into the chemicals, processing power, or functional effects needed in industry. So, their applications, performance, and proper selection directly affect the efficiency, energy consumption, lifespan, and overall cost-effectiveness of electrolysis equipment. This is also why they are widely used in industries like chlor-alkali, water treatment, chemical production, and surface treatment.
Among all application scenarios, producing sodium hypochlorite by electrolyzing brine is one of the most representative and widely used directions for MMO-coated titanium anodes. In an electrolytic cell, saltwater or seawater undergoes anodic electrolysis, with chlorine being released at the anode surface. The chlorine generated then hydrolyzes in water to form hypochlorite, resulting in a sodium hypochlorite solution with strong oxidizing and disinfecting properties. This process is widely applied in disinfecting tap water and wastewater plants, industrial circulating water treatment, swimming pool maintenance, hospital and public area sanitation, as well as seawater chlorination and antifouling systems on offshore platforms and ships.

Purchasing guide

Quality control(QC)
NAVI Titanium has made its tiered quality inspection data available for download, so customers can easily get the files they need to complete supply chain audits, project bids, factory inspections, and third-party compliance testing. Each COA is linked to a specific production batch to avoid mix-ups, effectively reducing risks like abnormal slot pressure or premature anode failure caused by impure raw materials or coating formula deviations.
| Certificate of Analysis | ||
| Titanium Base Material Suppliers: | Coating Precursor Suppliers: | COA of product: |
|
|
|
|


Manufacturing proces
The entire titanium anode production process is tightly interconnected: First, we carefully select high-purity titanium substrates and use laser cutting equipment for precise material cutting, processing them into plate, tube, or mesh blanks according to customer specifications. Next, the blanks go through surface pretreatment, where sandblasting and acid cleaning remove oxide scales and grease from the titanium surface, creating a rough, activated base that ensures excellent adhesion for the precious metal coating and prevents peeling later on.
A transparent and visible production process is the foundation of NAVI Titanium's commitment to product quality. You can click to see more details of our process and learn how we use precise manufacturing to provide global customers with cost-effective, long-lasting, customized titanium anodes.
 |
 |
 |
Selection Guide
All values are reference benchmarks for mass production. Final coating formulation, loading, tolerance and dimension will be customized according to electrolyte property, target reaction, continuous & peak current density and electrolyzer structure. ALT accelerated lifetime serves only for batch quality control comparison and shall NOT be linearly extrapolated to on-site service life.
| Parameter Category | Item | Reference Specification | Engineering Implication |
| Coating Formula & Reaction Selectivity | Ru:Ir Mass Ratio | High Cl₂ evolution:70:30Balanced:50:50High O₂ evolution:30:70Pure O₂ (Ir-Ta): Ru≈0 | Higher Ru ratio delivers better chlorine selectivity but weaker oxidation resistance; higher Ir ratio improves anti‑oxidation and service life with slightly higher chlorine evolution overpotential. Reaction competition dominates anode consumption rather than coating naming. |
| Coating Loading & Service Life Mapping | Coating LoadingDesign Working Current DensityEstimated Field Service Life | 6–8 g/m² @1–2 A/dm² → 3–5 years10–12 g/m² @3–4 A/dm² → 2–3 years15–18 g/m² @5–8 A/dm² →1.5–2 years≥20 g/m² for heavy duty | Practical service life is governed by coating loading divided by current density. Peak current density instead of average value determines degradation speed. Low loading paired with high surge current triggers premature coating spallation. |
| Interface & Microstructure | Surface MorphologyIntermediate Barrier LayerSubstrate Roughness RaThermal Shock Resistance | Mud‑cracked / Dense smoothIrO₂‑Ta₂O₅ / Ni interlayer0.4–0.8 μmNo peeling after thermal cycle at 450–550℃ | Most anode failures initiate at substrate-coating interface instead of coating bulk. Mud‑cracked texture enlarges active surface and facilitates bubble release; dense surface mitigates scaling under high salinity. Improper roughness weakens adhesion or creates hot spots. |
| Geometric Tolerance & Assembly | Plate FlatnessPlate BowElectrode Parallelism / Gap ToleranceMesh Hole ToleranceTransition Resistance of Welding Lead | ≤1 mm/m≤1.5 mm±0.5 mm±0.2 mm≤5 μΩ | Geometric precision controls inter‑electrode gap stability. Gap inconsistency induces uneven current distribution, local hotspots and hidden long‑term power waste. High contact resistance on terminals accumulates extra heat and power loss. |
| Electrochemical Performance & Accelerated Test | Chlorine Evolution OverpotentialCurrent Efficiency for HypochloriteALT Accelerated Life | 1.05–1.15 V (1 kA/m², saturated NaCl, vs SCE)85–92%Hundreds to thousands of hours under overload current | Lower overpotential reduces specific energy consumption. Efficiency varies with salinity, temperature, pH and gas coverage. ALT test is a QC indicator and needs empirical de‑rating before field prediction. |
| Anode Geometry & Cell Matching | Plate AnodeExpanded / Woven Mesh AnodeTubular / Cylindrical AnodeRod Anode | Side length:300–1200 mmMesh opening:4–15 mmDiameter:φ20–φ100 mmCustom length | Plate for filter‑press electrolyzer and hypochlorite production; mesh for high‑flow cooling water and marine electrochlorination; tubular for tubular electrolysis skids; rod for special electrolysis and plating. |
During transportation, friction, local pressure, salt spray pre-corrosion, and moisture penetration can all cause invisible micro-cracks and partial coating loss. This table covers the transport risks, packaging grades, carrier restrictions, and inspection blind spots that OEMs, system integrators, and international engineering buyers of MMO coated titanium anode for electrolysis cell often overlook.
| Category | Item | Reference Spec / Requirement | Hidden Risk & Engineering Note |
| Coating Surface Sensitivity | Allowable surface contact pressure | ≤0.03 MPa on coated working face | The cracked MMO catalytic layer is brittle. Minor concentrated point load creates invisible microcracks. Cracks propagate rapidly under electrolyte and current, causing titanium substrate passivation and early failure. Chipping is not the only failure mode. |
| Friction tolerance | Dry surface-to-surface contact & friction prohibited | Low surface hardness of mixed metal oxide; dry friction strips noble metal active ingredients. Many transit damages come from continuous rubbing inside packages instead of heavy impact. | |
| Pre-corrosion tolerance in transit | Avoid exposure to salt spray, acid mist and condensation before installation | Unenergized MMO coating suffers static chemical corrosion under humid salt atmosphere, weakening substrate-coating bonding layer. Goods may look intact on arrival yet with shortened service life. | |
| Packaging & Inner Protection | Separator material | EPE foam / acid-free kraft paper. Sawdust, sulfur-containing foam and recycled corrugated are banned | Common fillers release organic acid and sulfur compounds. Volatiles trapped inside sealed boxes contaminate active sites and raise cell voltage after commissioning, hard to trace. |
| Moisture barrier option | Standard: Sealed PE bag + desiccantOcean shipment: Aluminium foil vacuum bag + humidity indicator | Normal PE film fails against condensation caused by day-night temperature cycling inside containers. Vacuum packaging is designed for long sea transit. | |
| Supporting bearing point | Support only on uncoated titanium frame edges. Never bear load on coated working surface | Improper support creates alternating shear stress between coating and substrate during vibration, a major hidden cause of later peeling. | |
| IPPC wooden pallet | Sea freight: IPPC heat-treated markAir freight: Non-wood packing preferred | Untreated timber brings mold and moisture risk besides customs non-compliance. VOC released from raw wood may contaminate electrode surfaces. | |
| Outer Crate & Pallet | Stacking limit | Max 2 layers for wooden crates; no direct stacking on anode cartons | Overstacking induces permanent bow deformation. Excessive bow violates geometric tolerance, resulting in uneven inter-electrode gap and local hot spots inside electrolysis cell. |
| Shipping marks | Fragile, No Rolling, Do Not Stack, No Scratch on Coated SurfaceClear marking for working side | Generic fragile labels do not alert handlers. Coated surfaces are often dragged randomly without awareness. |
Notes
Most failures are blamed on coating quality, but a majority of field failures actually result from improper installation, current management and maintenance practice. This table focuses on overlooked precaution dimensions for electrolyzer OEMs, system integrators, operators and buyers
| Category | Item | Reference Rule / Note | Cold Hidden Risk |
| Installation & Pre-charge | Never energize without electrolyte | Confirm cell fully flooded before energizing; strictly no dry running | Dry running creates localized high temperature in seconds, burning coating and passivating titanium substrate. Many first-year failures originate from this, often invisible to visual check. |
| Electrode polarity & orientation | Confirm wiring and coated side facing; reverse polarity destroys coating quickly | MMO coating is designed for anodic use only. Long-term operation as cathode under reducing environment rapidly degrades coating and contaminates the cell. | |
| Gap & flatness re-check | Verify gap within ±0.5 mm and bow ≤1.5 mm after transport | Transit deformation causes uneven gap, localized current overload and hot spots, accelerating local coating loss. A common root cause of unexplained local failure. | |
| Deburring & cleaning | Remove burrs, clean oil, remove metal particles from cell | Metal debris between electrodes creates micro short-circuit, sparks and local high temperature, scorching coating; oil impairs wetting and current uniformity. | |
| Electrical Operation | Current ramp-up | Ramp current gradually, not instant full load | Sudden full load induces thermal shock on coating interface and microcracks. Gradual ramp significantly extends life. |
| Peak current density control | Design against peak, not average; avoid repeated surge | Repeated surge current is the main cause of coating spallation and premature failure. Peak-based design is the most overlooked operational point. | |
| Polarity reversal only if designed | Reverse only on cleaning-designed systems; random reversal on non-designed anode damages coating | Unsupported polarity reversal destroys coating structure within hours. Scale removal should follow designed reversal or chemical cleaning. | |
| Shutdown & idle | Avoid partially energized state and repeated start-stop cycling | Long idle immersion and repeated start-stop alternating current accelerate interface fatigue and static chemical corrosion. | |
| Electrolyte & Process | Impurity control | Control suspended solids, oil, heavy metals; avoid sudden salinity change | Particles abrade coating; oil poisons active sites; salinity swing shifts chlorine/oxygen competition and working point. |
| Chlorine load balance | Match production to demand; avoid sustained overproduction | Overproduction wastes energy, raises by-products and downstream corrosion pressure - both economic and compliance risk. | |
| Temperature stability | Avoid drastic frequent temperature swings | Mismatched thermal expansion between MMO and Ti substrate triggers interfacial debonding; excessive temperature accelerates consumption. | |
| Maintenance & Inspection | Coating inspection method | Visual + non-destructive tapping/thickness check; never scrub with hard tools | Mechanical scraping during maintenance is a frequent secondary damage source. Track bow, cell voltage and current efficiency trend as life judgment. |
| Scale removal method | Designed chemical cleaning or polarity reversal; never hammer/pry | Forced impact to strip scale simultaneously shatters brittle MMO coating, causing large-area detachment. | |
| Record baseline & trend | Record initial bow, voltage, current efficiency; track trend | Judge life by trend data instead of "looks fine", enabling scheduled replacement and avoiding unplanned shutdown. | |
| Storage & Spare | Storage environment | Dry, ventilated, non-salt-spray indoor area; sealed with desiccant | Humid salt atmosphere triggers static chemical corrosion before energizing; interface weakens first, shortening on-site life. |
| Spare anode rotation | Rotate spares regularly; do not idle one anode for years | Idle spare coating degrades during storage. Rotation keeps on-line anodes in healthy condition. |
Frequently Asked Questions
Can custom anodes be reserved with margin for future recoating?
+
-
Yes. NAVI Titanium designs substrate margin and terminal protection structure during customization, instead of only designing for initial working conditions. Many buyers overlook that qualified titanium substrates can be stripped and recoated to cut long-term procurement costs. We control the sandblasting etching depth according to your cell maintenance interval and target service life, preventing substrate thinning and unstable conductivity after multiple recoats. We can mark recoatable versions separately in quotations to distinguish from disposable anodes.
Does electrolyzer flow field affect coating uniformity?
+
-
Yes, this is often overlooked in custom orders. Electrolyte flow speed, bubble discharge routes and internal eddy current cause offset of local current density and premature coating failure. Beyond dimensional machining, NAVI adjusts active area layout based on your cell structure and liquid distribution. Gradient coating loading is applied on edges and dead zones to avoid overload and consistent ageing across the whole anode.
Is custom adaptation available for reverse polarity operation?
+
-
Standard MMO coatings cannot withstand frequent polarity switching. For periodic reverse-polarity processes such as cell self-cleaning, we customise multi-layer transition coating systems to strengthen coating-substrate adhesion and resist peeling. Please supply reverse cycle duration and switching frequency. We will not use standard Ru-Ir or Ir-Ta recipes, but tune thermal decomposition layers and precursor ratios for polarity reversal scenarios.
Can accelerated life testing be offered alongside small-batch custom orders?
+
-
Available even for 1–3 prototype units. NAVI Titanium provides lab accelerated electrolysis tests with polarization curves and accelerated life reports, not only material certificates. Ideal for new-process piloting and import replacement benchmarking, helping you predict degradation risks before cell installation and cut debugging losses.
Can custom anode lugs match existing electrolyzer sealing assemblies?
+
-
Yes. Terminals, weld zones and insulation are frequent pain points during retrofitting. We design conductive outlets matching your existing gaskets and PTFE insulators. Heat-affected zones from welding are controlled to avoid thermal damage to nearby seals. We check assembly tolerances and creepage distances at drawing stage for direct installation without on-site cell modification.
Hot Tags: mmo coated titanium anode for electrolysis cell, China mmo coated titanium anode for electrolysis cell manufacturers, suppliers, factory, low overpotential coated titanium anode, MMO Coated Titanium Anodes, Platinum Coated Titanium Electrodes, titanium anode for metal recovery, Titanium Anode for Water Heater, Titanium Cathode